




Compressed Air Purity Monitoring in Automated Paint Shops
In Highly Automated Painting Processes


Application
Compressed air quality and purity monitoring in highly automated painting processes

Goal
Ensure paint process quality by monitoring the compressed air purity

Customer
Car Manufacturer / Automated Paint Shop Manufacturer

Sector
Automotive Industry
Overview and Challenges
1. Overview
In a modern paint shop, painting quality depends heavily on the quality of the compressed air. During the painting process, paint is injected into compressed air and atomized into a fine, even mist as it exits the nozzle. The tiny paint particles repel each other and adhere evenly to the painted surface. However, impurities in the compressed air can cause the particles to clump together, leading to uneven coverage, coating defects, and increased waste.
2. Challenge of the Customer
To prevent these issues, paint equipment manufacturers define strict compressed air purity requirements. These requirements focus on dew point, oil vapor content, and particle concentration. In many installations, however, the end customer is responsible for maintaining air quality. As a result, paint shop manufacturers often have limited visibility into actual operating conditions. Diagnosing coating defects can therefore become more difficult and time-consuming.
3. Solution and Implementation
How SUTO iTEC Compressed Air Quality Measurement Solutions are used to Ensure the Quality of Painting Results?
The only way to ensure a consistent high-quality painting process is by monitoring the compressed air purity so painting equipment manufacturers are now starting to integrate air purity measurement tools directly into their machines to monitor the supplied air quality.
Two solutions are designed to be used in such applications:
- Supply Side – A Stationary Compressed Air Purity Analyzer (SUTO iTEC S601) is installed, providing a permanent monitoring of dew point, oil vapor content and particle concentration in the compressed air.
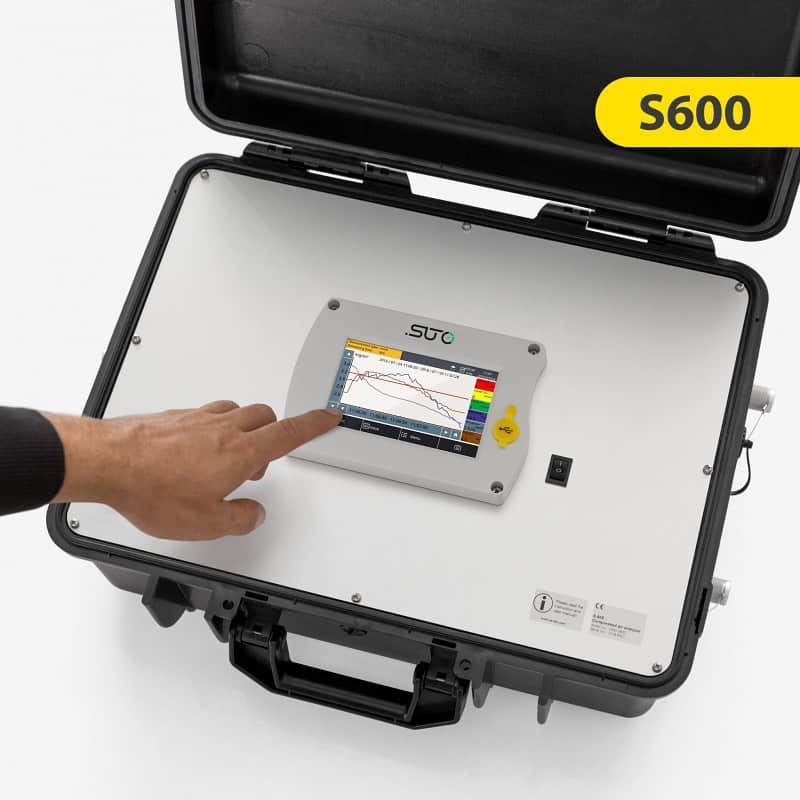
- Demand Side – Equipped with a Portable Compressed Air Purity Analyzer (SUTO iTEC S600), on-site process engineers are enabled to test the compressed air purity as an initial quality check after the installation and then perform ongoing regular checks whenever needed.

4. Results
The SUTO iTEC compressed air purity solutions helped ensure stable painting quality, enabled continuous compliance monitoring, reduced troubleshooting efforts, and strengthened confidence in paint shop operations.

24/7 Quality Monitoring
Continuous measurement of dew point, oil vapor, and particle concentration provided real-time visibility into compressed air purity across the painting process.

100% Purity Verification
On-site audits and routine inspections enabled operators to verify compressed air quality against defined paint shop requirements before quality issues could impact production.

Proactive Fault Detection
Early identification of contamination risks helped maintenance teams address air quality problems before they affected coating consistency or caused product defects.

Reliable Paint Process
Permanent monitoring and regular purity checks improved confidence in production quality, supporting consistent coating performance and reducing the risk of rework.
5. Conclusion
Paint shop process quality can only be ensured if the supplied compressed air meets certain purity standards. Contamination in the compressed air can lead to production failures and create damage on the product and the reputation.
Constant monitoring and regular purity checks help operators as well as paint shop manufacturers to prevent damages and ensure high quality production output.
6. Products in Use
The following SUTO iTEC solutions were deployed to monitor dew point, oil vapor content, and particle concentration, helping ensure the compressed air purity required for consistent painting quality.
Related Case Studies
Explore more success stories on compressed air quality monitoring, process optimization, and quality-critical industrial applications.

Precise Compressed Air Quality Monitoring for ZEISS

Flawless Paint Quality through Advanced Compressed Air Quality Monitoring

Ensuring High Compressed Air Quality Standards in the Photovoltaic Industry
Ensure Painting Quality with Continuous Compressed Air Purity Monitoring
Improve paint process reliability, enhance product quality, and prevent costly rework with SUTO compressed air purity monitoring solutions.
